Indexable inserts
CNC Turning Inserts
Standard geometries for turning, finishing, profiling and roughing
The Qeviora range brings together widely used CNC turning insert designations: CNMG, DNMG, TNMG, SNMG and VNMG. Each family may include several chipbreakers, grades and coatings selected according to workpiece material, setup stability and the required surface finish.
Indicative data — technical validation required

Designations
Choose a geometry
Five ISO turning families and one APKT insert presented separately for indexable milling.

CNMG
CNMG
80° negative rhombic
ISO P · M · K · N
View specifications
DNMG
DNMG
55° negative rhombic
ISO P · M · K · S
View specifications
TNMG
TNMG
60° negative triangular
ISO P · M · K · N
View specifications
SNMG
SNMG
90° negative square
ISO P · M · K · S
View specifications
VNMG
VNMG
35° negative rhombic
ISO P · M · K · H
View specifications
APKT
Milling applicationAPKT Indexable Insert — Milling Application
Positive insert for indexable milling cutters
View specifications
CNMG
CNMG
80° negative rhombic insert widely used for longitudinal turning, facing, semi-finishing and medium roughing. Its robust geometry is suited to stable setups and provides several usable cutting edges depending on the toolholder.
Example: CNMG 120408
- C: 80° rhombic
- N: 0° clearance, negative insert
- M: tolerance class
- G: clamping / geometry type
- 12: nominal size
- 04: thickness
- 08: 0.8 mm nose radius
Applications
- Longitudinal turning
- Facing
- Semi-finishing
- Medium roughing
| Qeviora code | Coating | ISO | Vc m/min | f mm/rev | 订购 |
|---|---|---|---|---|---|
| QP4225 | CVD gold | P | 140–220 | 0.12–0.35 | |
| QM2015 | PVD bronze | M | 90–160 | 0.1–0.28 | |
| QK1010 | PVD anthracite | K | 160–260 | 0.12–0.35 | |
| QN0520 | Polished / uncoated | N | 300–900 | 0.08–0.3 |
Indicative starting values. Adjust parameters to the exact workpiece grade, hardness, chipbreaker, nose radius, depth of cut, setup rigidity, machine power, toolholder and coolant strategy. Trial validation is mandatory before final commercial publication.
DNMG
DNMG
55° negative rhombic insert suited to profiling, finishing and operations requiring better accessibility than a CNMG insert.
Example: DNMG 150608
Applications
- Profiling
- Versatile turning
- Finishing
- Semi-finishing
| Qeviora code | Coating | ISO | Vc m/min | f mm/rev | 订购 |
|---|---|---|---|---|---|
| QP4215 | CVD gold | P | 150–230 | 0.1–0.3 | |
| QM3215 | PVD bronze | M | 90–150 | 0.08–0.22 | |
| QK1110 | PVD anthracite | K | 170–260 | 0.1–0.3 | |
| QS2310 | PVD nano | S | 50–90 | 0.06–0.18 |
Indicative starting values. Adjust parameters to the exact workpiece grade, hardness, chipbreaker, nose radius, depth of cut, setup rigidity, machine power, toolholder and coolant strategy. Trial validation is mandatory before final commercial publication.
TNMG
TNMG
60° negative triangular insert offering good versatility in general turning and several usable cutting edges.
Example: TNMG 160408
Applications
- General turning
- Facing
- Profiling
- Semi-finishing
| Qeviora code | Coating | ISO | Vc m/min | f mm/rev | 订购 |
|---|---|---|---|---|---|
| QP4225 | CVD gold | P | 150–240 | 0.12–0.32 | |
| QM2215 | PVD bronze | M | 100–160 | 0.1–0.25 | |
| QK3310 | PVD anthracite | K | 170–280 | 0.12–0.32 | |
| QN0515 | Polished / uncoated | N | 350–950 | 0.1–0.35 |
Indicative starting values. Adjust parameters to the exact workpiece grade, hardness, chipbreaker, nose radius, depth of cut, setup rigidity, machine power, toolholder and coolant strategy. Trial validation is mandatory before final commercial publication.
SNMG
SNMG
Robust 90° negative square insert mainly intended for roughing, high chip loads and rigid setups.
Example: SNMG 120408
Applications
- Roughing
- Stable longitudinal turning
- High depths of cut
- Moderate interrupted cut depending on grade
| Qeviora code | Coating | ISO | Vc m/min | f mm/rev | 订购 |
|---|---|---|---|---|---|
| QP4415 | CVD gold | P | 120–210 | 0.18–0.45 | |
| QM2415 | PVD bronze | M | 80–140 | 0.14–0.35 | |
| QK1410 | PVD anthracite | K | 150–250 | 0.18–0.45 | |
| QS2315 | PVD nano | S | 45–80 | 0.1–0.25 |
Indicative starting values. Adjust parameters to the exact workpiece grade, hardness, chipbreaker, nose radius, depth of cut, setup rigidity, machine power, toolholder and coolant strategy. Trial validation is mandatory before final commercial publication.
VNMG
VNMG
35° negative rhombic insert designed for finishing, precision profiling and access to narrow features. Its tip is less robust than a CNMG or DNMG and requires a stable setup.
Example: VNMG 160404
Applications
- Finishing
- Profiling
- Low depths of cut
- Complex geometries
| Qeviora code | Coating | ISO | Vc m/min | f mm/rev | 订购 |
|---|---|---|---|---|---|
| QP4210 | CVD gold | P | 160–240 | 0.06–0.22 | |
| QM2210 | PVD bronze | M | 100–170 | 0.05–0.18 | |
| QK1210 | PVD anthracite | K | 180–270 | 0.06–0.22 | |
| QH0610 | PVD nano | H | 45–85 | 0.03–0.12 |
Indicative starting values. Adjust parameters to the exact workpiece grade, hardness, chipbreaker, nose radius, depth of cut, setup rigidity, machine power, toolholder and coolant strategy. Trial validation is mandatory before final commercial publication.
APKT Insert for Indexable Milling
The APKT designation refers to a positive insert commonly used in indexable milling cutters for face milling, contouring, shoulder milling and other versatile milling operations.
Example: APKT 1604
Applications
- Shoulder milling
- Face milling
- Contouring
- Slotting depending on cutter
- Versatile milling
| Qeviora code | Coating | ISO | Vc m/min | fz mm/tooth | ap | 订购 |
|---|---|---|---|---|---|---|
| QP4215 | CVD gold | P | 120–220 | 0.08–0.2 | per cutter | |
| QM2215 | PVD bronze | M | 70–140 | 0.06–0.16 | per cutter | |
| QK1210 | PVD anthracite | K | 140–240 | 0.08–0.22 | per cutter | |
| QN0515 | Polished / uncoated | N | 250–600 | 0.1–0.3 | per cutter | |
| QS2610 | PVD nano | S | 35–70 | 0.04–0.12 | per cutter |
APKT values depend strongly on cutter diameter, tooth count, lead angle, overhang, radial engagement and axial depth of cut.
Indicative starting values. Adjust parameters to the exact workpiece grade, hardness, chipbreaker, nose radius, depth of cut, setup rigidity, machine power, toolholder and coolant strategy. Trial validation is mandatory before final commercial publication.
ISO material groups
Classification cues to guide grade and coating selection.
Coating families
Provisional visual families. Exact chemical composition remains to be confirmed by supplier certificate.
CVD gold
Wear resistance for stable applications.
PVD bronze
Balance of toughness and wear resistance.
PVD anthracite
Thermal stability and targeted material use.
PVD nano
Toughness and finishing depending on grade.
Polished / uncoated
Aluminum and non-ferrous materials.
Technical warning: visuals, designations and parameters are indicative only. They are not a guarantee of performance, stock, lead time or validated chemical composition.
turning-inserts

联系
谈谈您的工业项目
我们的团队随时了解您的挑战,并按绩效目标提供适配的支持。
(+212) 06 38 38 11 46
电话
(+212) 06 38 38 11 46
电子邮件
admin@qeviora.com
报价
devis@qeviora.com

网站
www.Qeviora.com
位置
Qeviora 布局
以贴近客户为目标的战略布局。
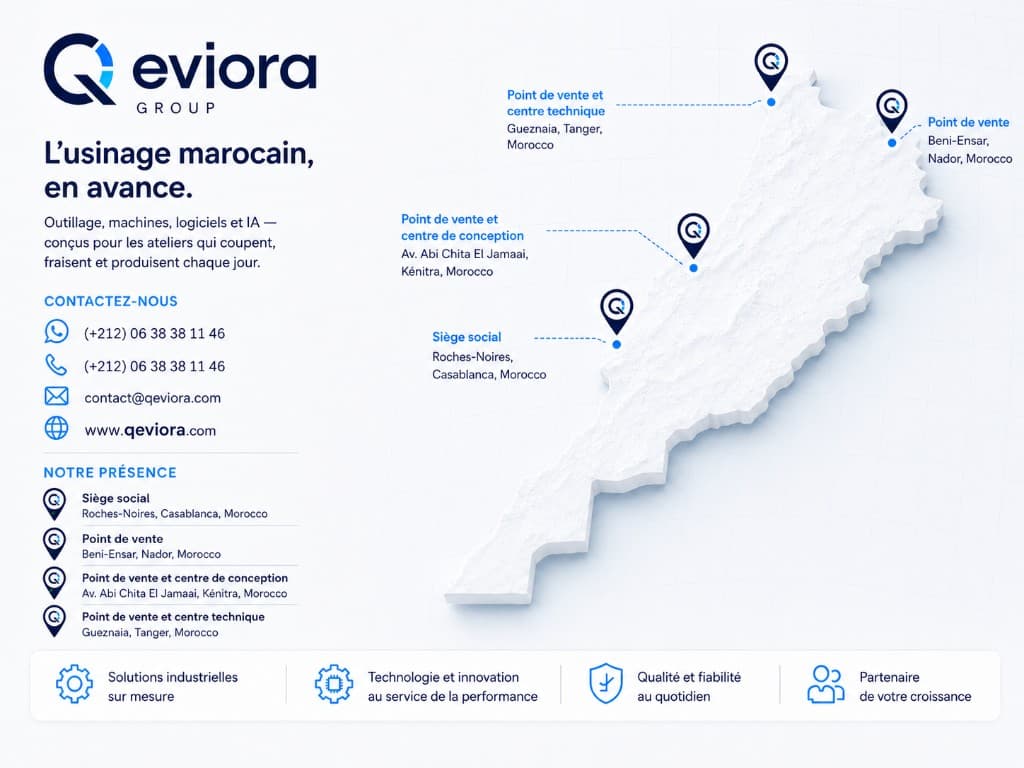
总部
Roches-Noires, Casablanca, Morocco
销售点与设计中心
Av. Abi Chita El Jamaai, Kénitra, Morocco
销售点与技术中心
Gueznaia, Tanger, Morocco
销售点
Beni-Ensar, Nador, Morocco