Solid carbide ball nose end mills
Solid Carbide Ball Nose End Mills
Qeviora solid carbide ball nose end mills are designed for 3D surface machining, complex contours, radii, moulds, dies and components requiring a consistent surface finish. Their hemispherical cutting end supports contour milling, semi-finishing, finishing and machining of difficult-to-reach areas.
Die bestellbare Standardreihe umfasst die Durchmesser D1, D2, D3, D4, D5, D6, D8, D10 und D12. Der Kugelradius entspricht der Hälfte des Schneiddurchmessers: z. B. entspricht D6 dem Wert R3. Der Schaftdurchmesser folgt der Qeviora-Standardmatrix (D1–D3 → d4; D4–D5 → d6; ab D6 → d = D).
All cutting values shown on the website must be identified as indicative starting values. They must be adjusted according to the exact workpiece grade and hardness, holder, runout, tool overhang, machine rigidity, toolpath, radial and axial engagement, and cooling strategy.
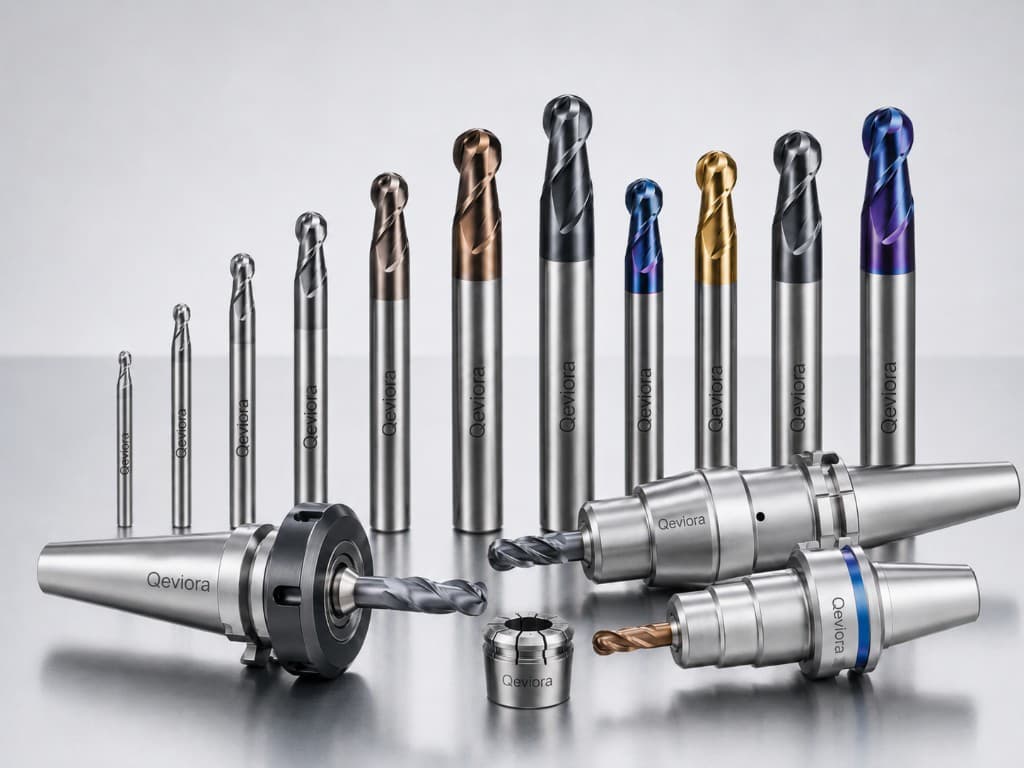
Standardreihe
Durchmesser wählen
Wählen Sie den Schneiddurchmesser. Der passende Schaftdurchmesser wird automatisch gemäß der Qeviora-Standardmatrix gesetzt.
- Schneiddurchmesser
- Ø1 mm
- Schaftdurchmesser
- Ø4 mm
- Referenz
- QCT-BN-D01-S04
Filter by ISO group
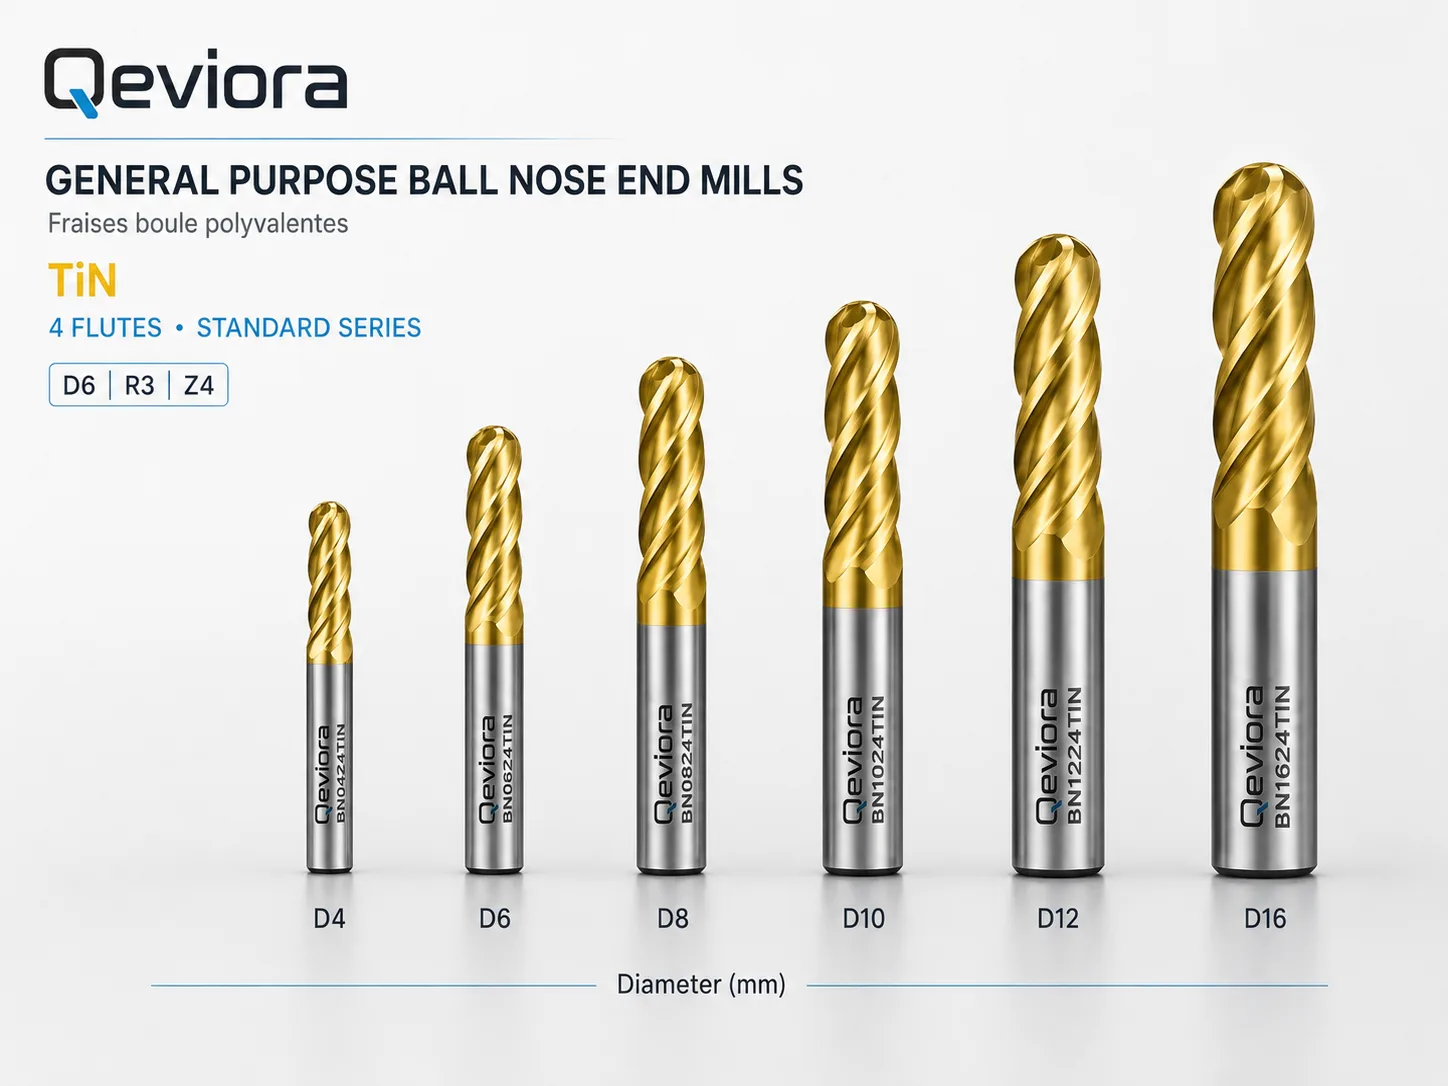
General purpose
General Purpose
General operations, contouring, semi-finishing and finishing — ISO P / M / K, secondary N.
ISO: P · M · K · N · Geometry: D6 | R3 | Z4
View datasheet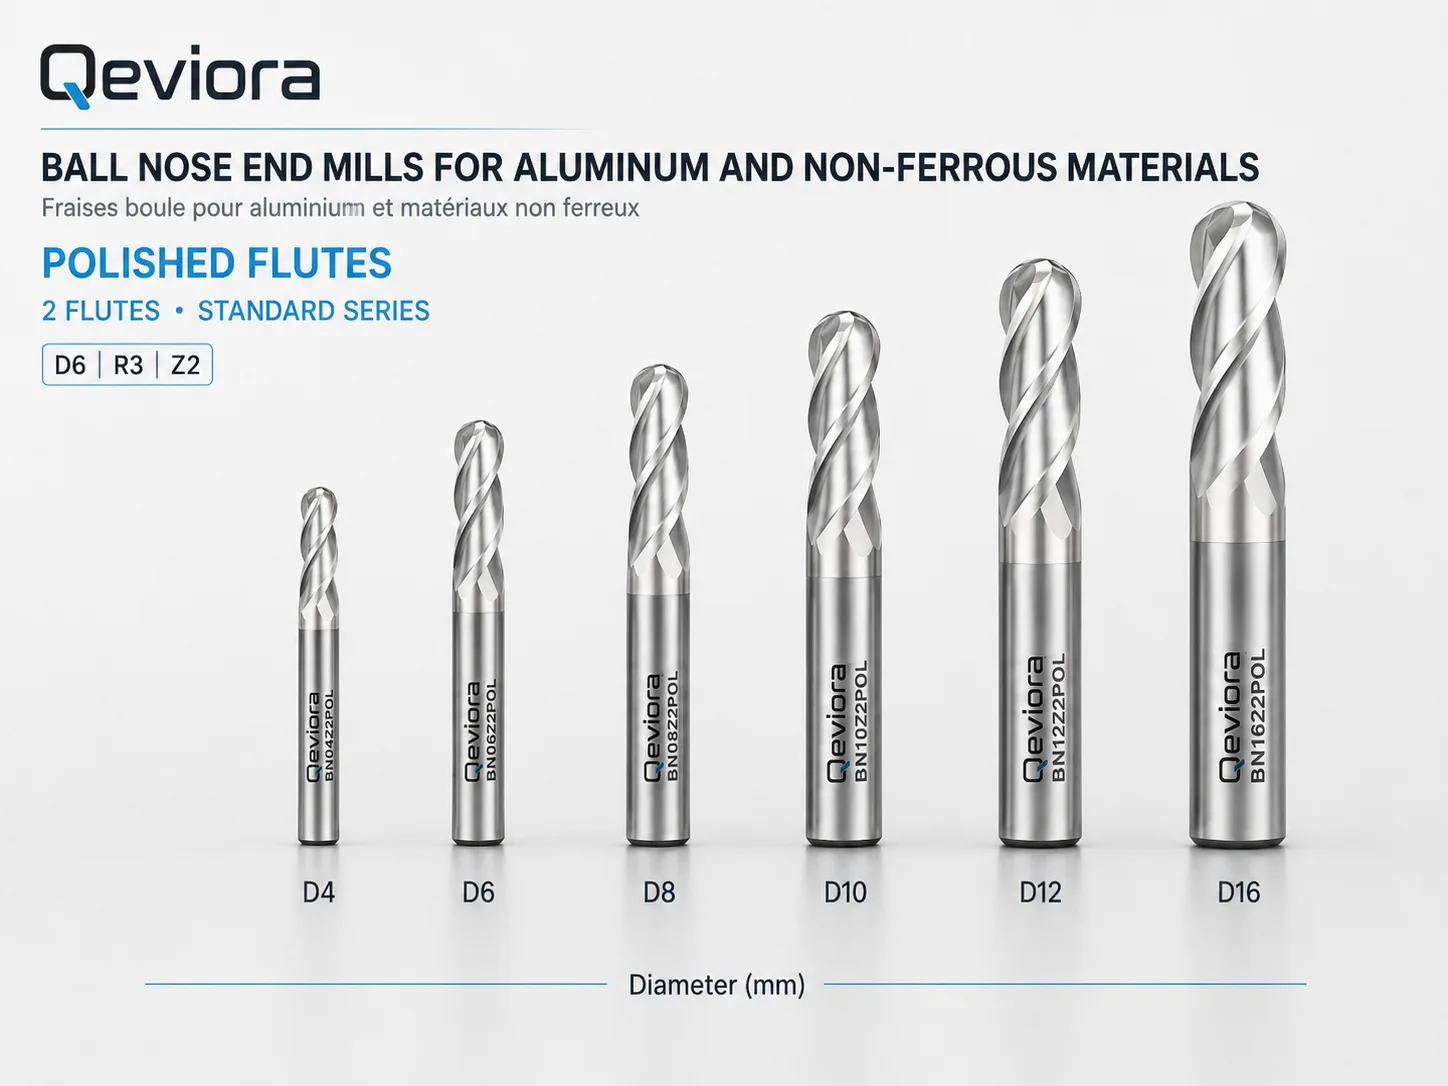
Aluminum / non-ferrous
Aluminum and Non-Ferrous Materials
Wrought or cast aluminum and non-ferrous alloys — ISO N, Z2 polished flutes.
ISO: N · Geometry: D6 | R3 | Z2
View datasheet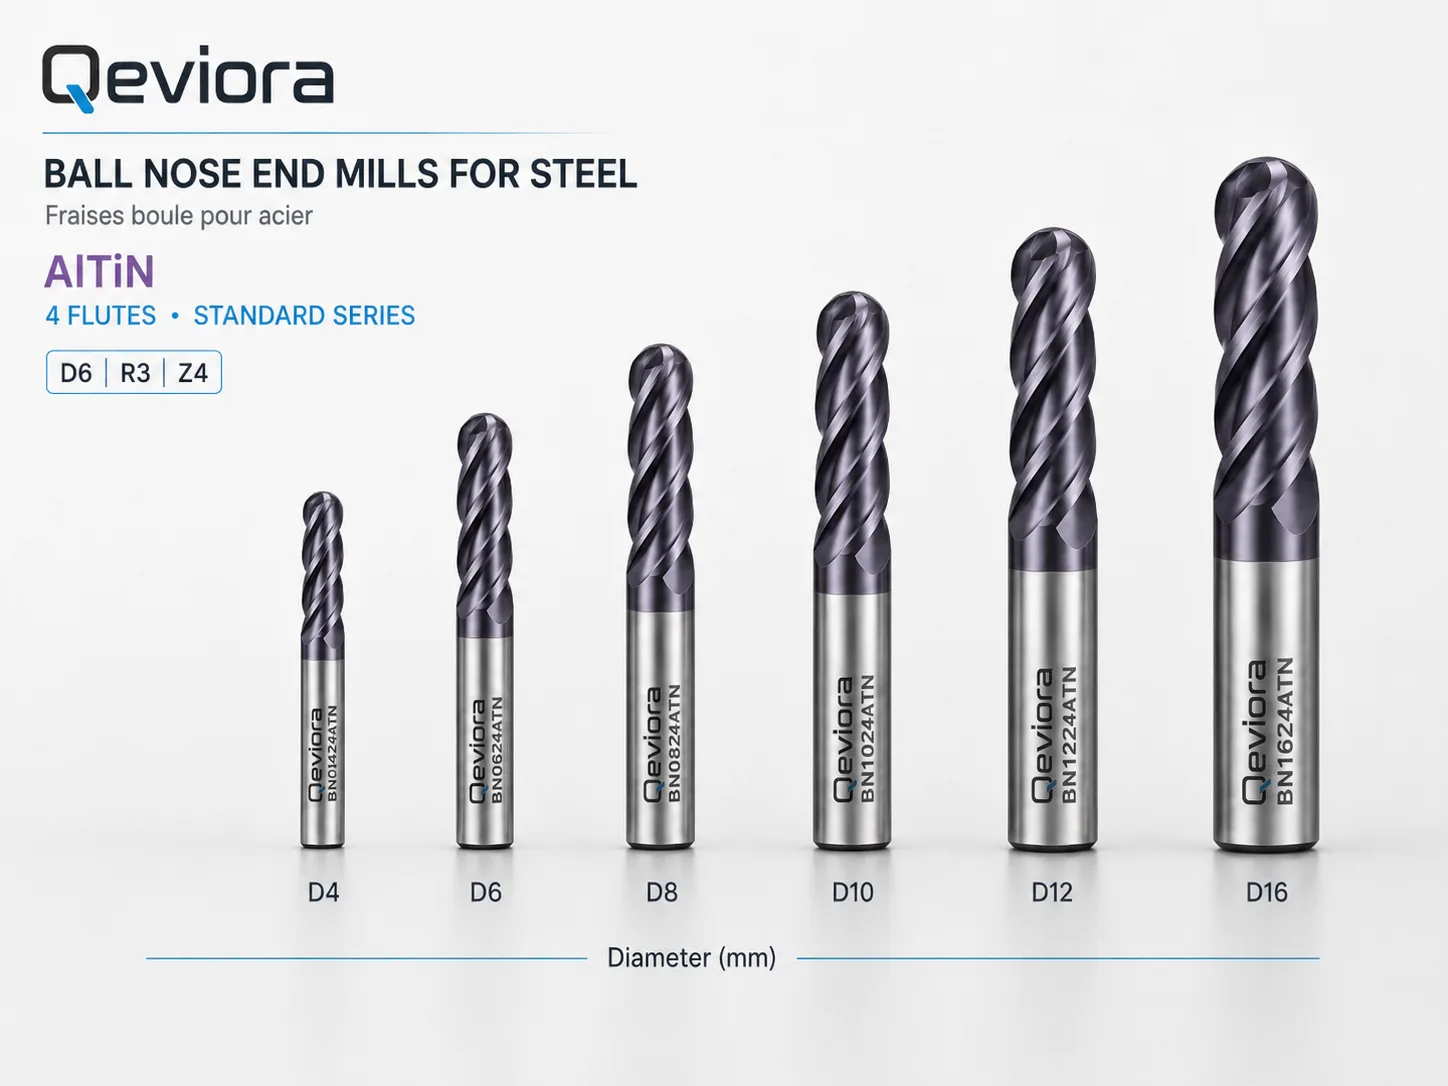
Steel
Steel
Unalloyed and alloy steels — ISO P, Z4, AlTiN visual finish.
ISO: P · Geometry: D6 | R3 | Z4
View datasheet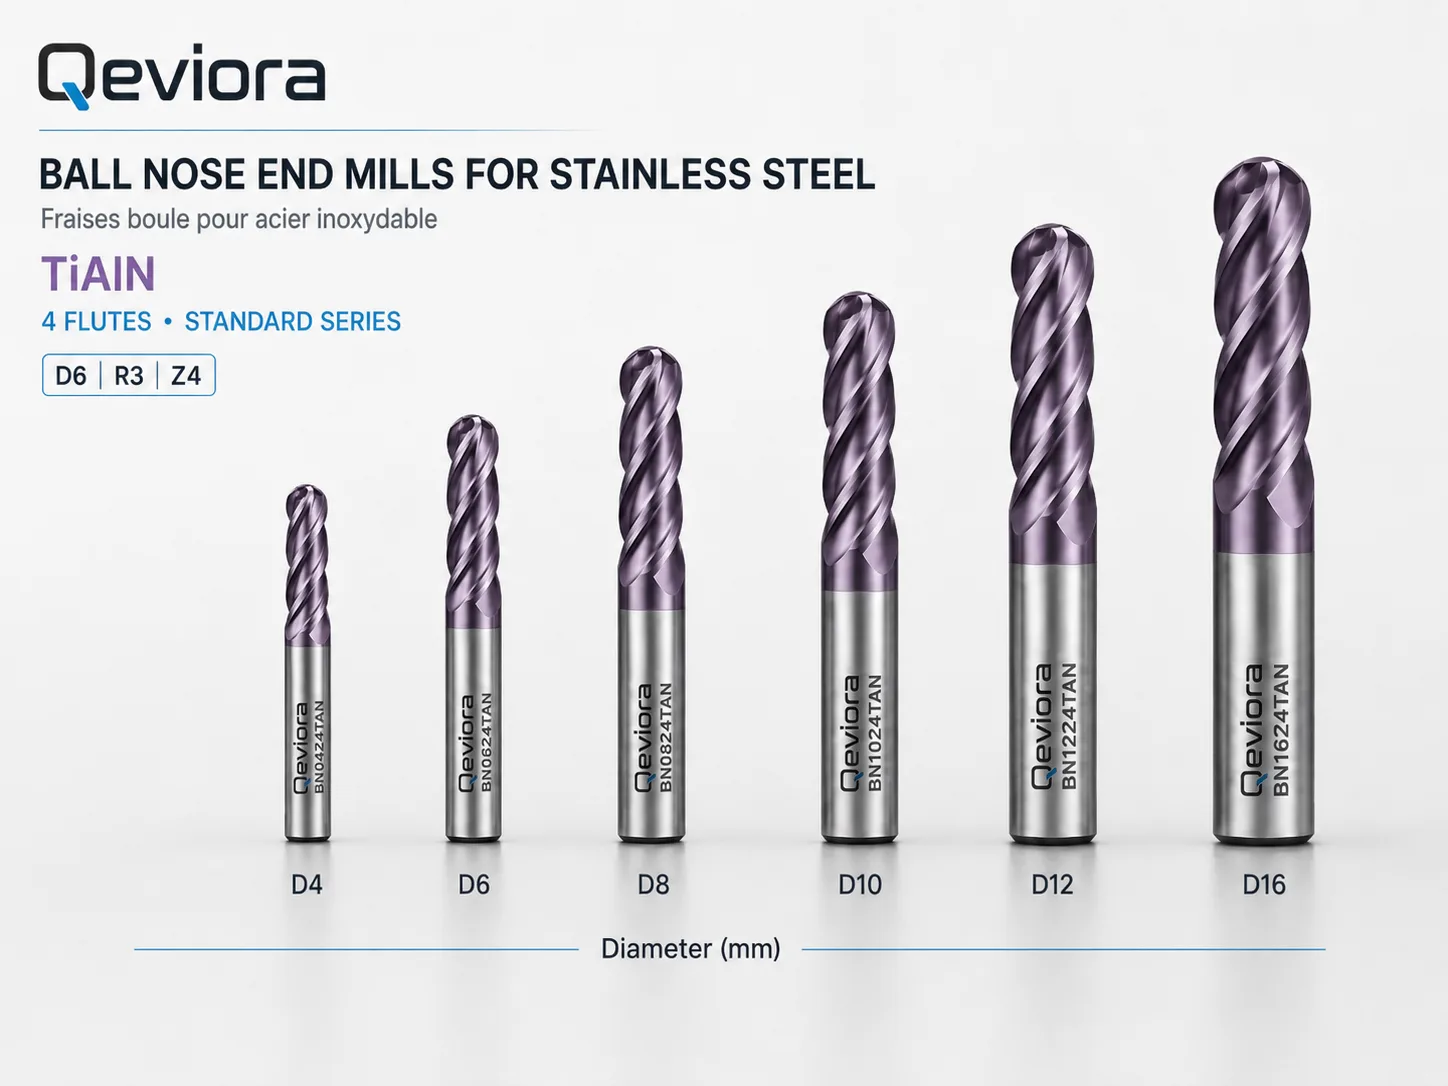
Stainless steel
Stainless Steel
Ferritic, martensitic, austenitic and duplex stainless — ISO M, subject to adaptation.
ISO: M · Geometry: D6 | R3 | Z4
View datasheet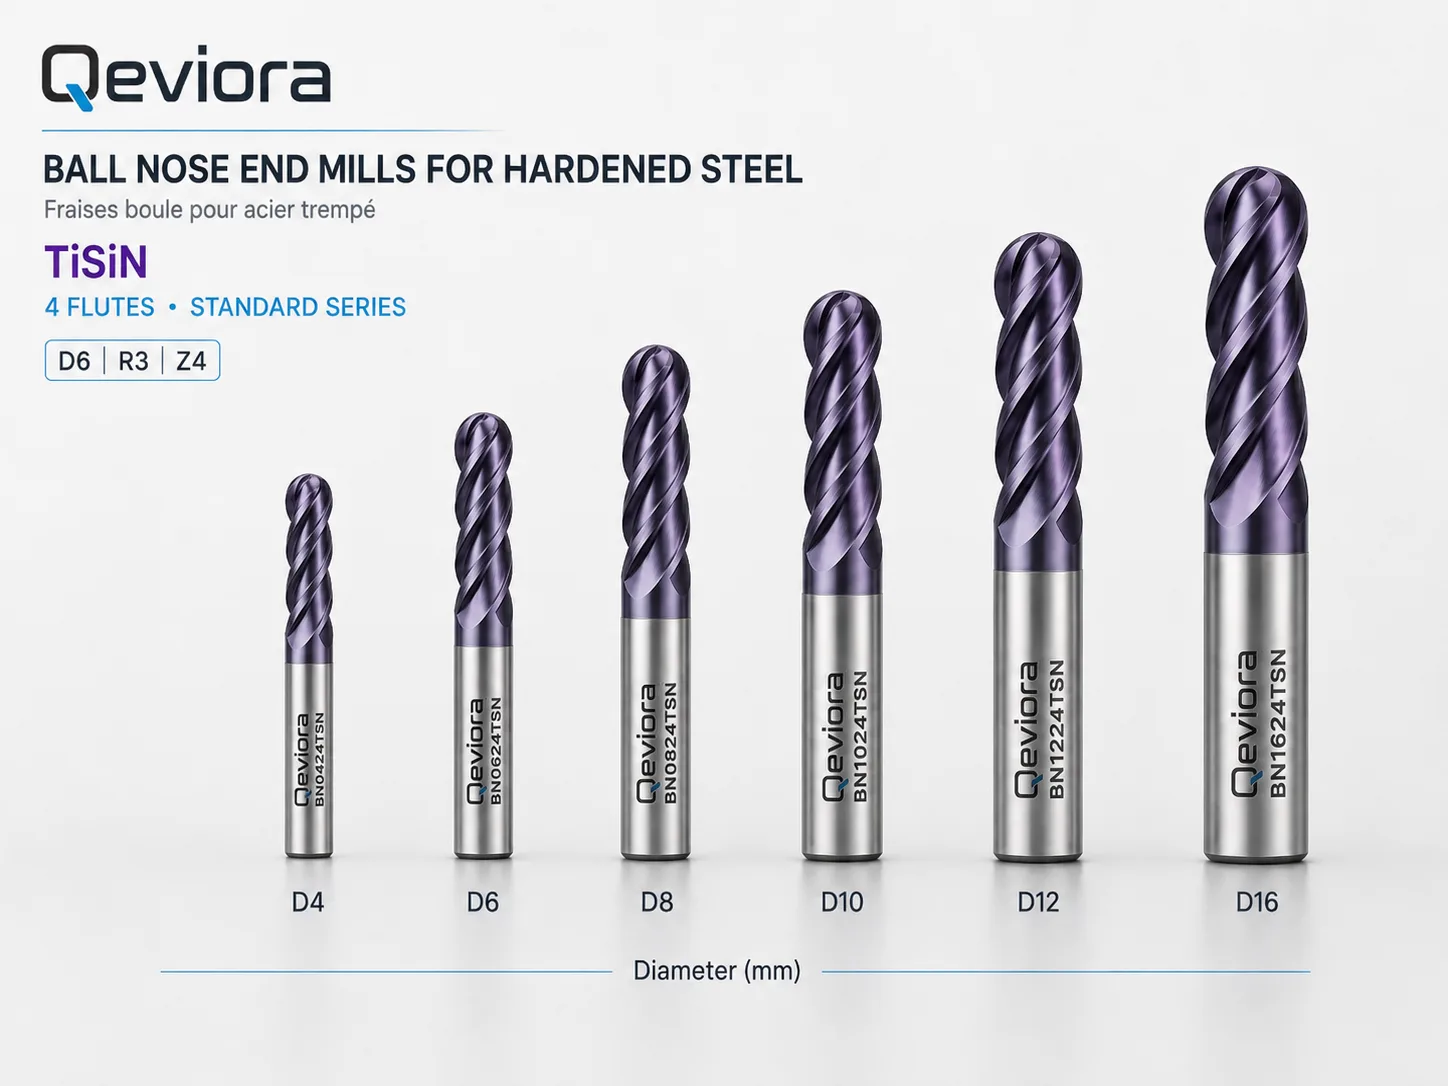
Hardened steel
Hardened Steel
3D finishing of hardened materials — ISO H, Z4. Application cue 48 to 65 HRC.
ISO: H · Geometry: D6 | R3 | Z4
View datasheet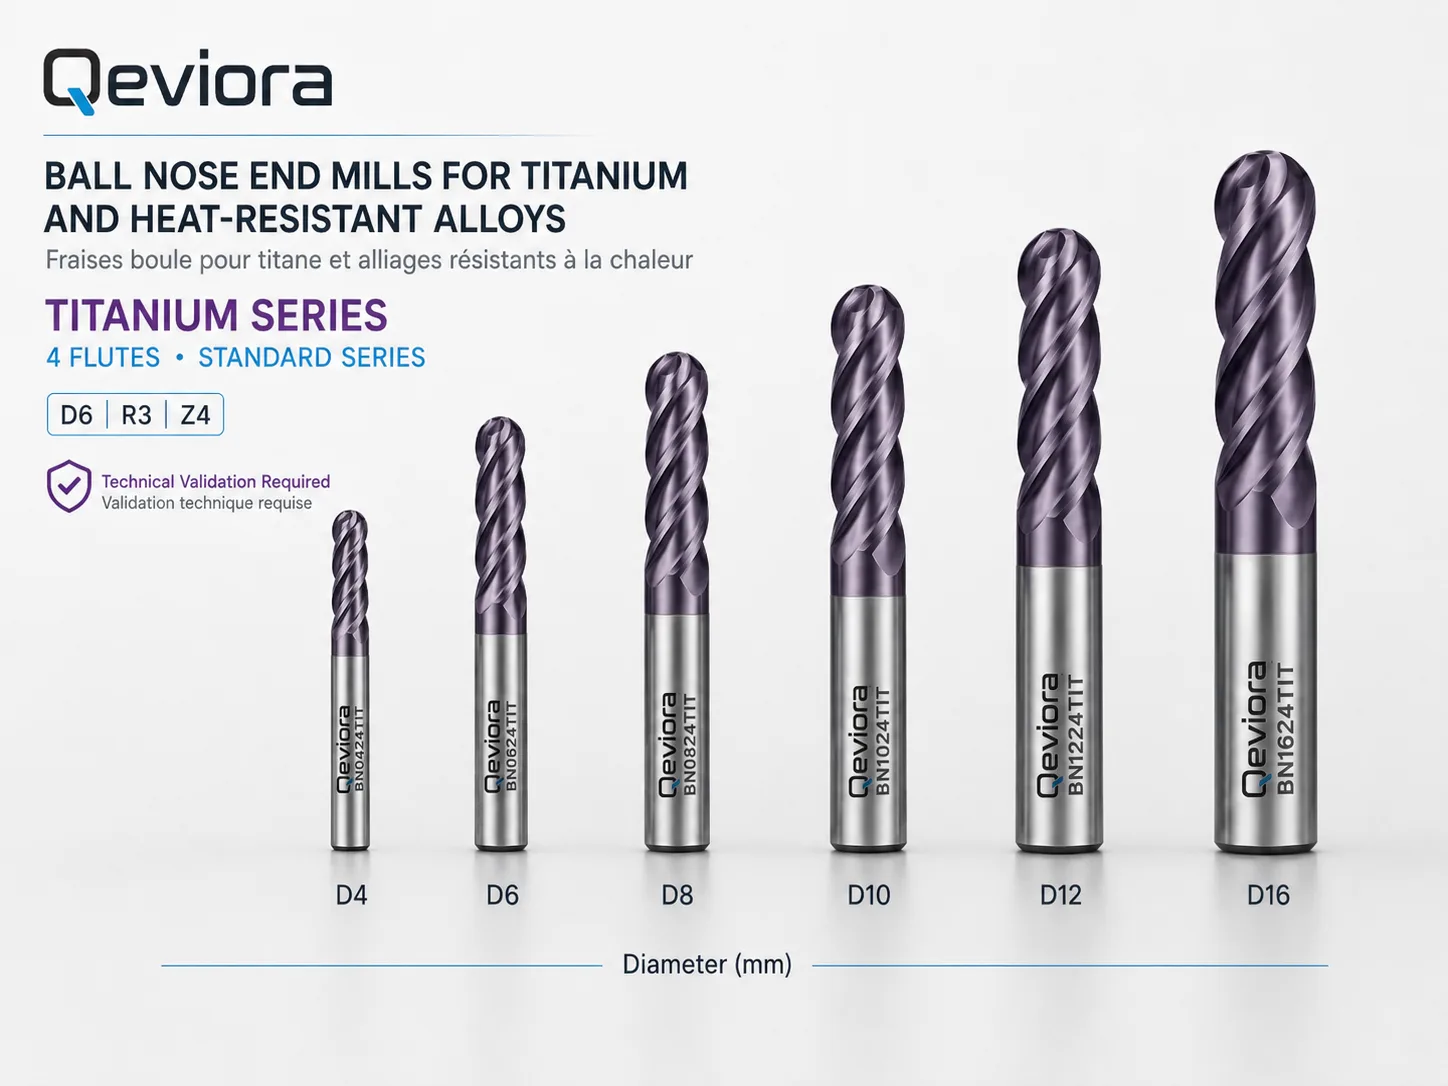
Titanium / heat-resistant
Titanium and Heat-Resistant Alloys
Titanium, nickel alloys and heat-resistant materials — ISO S. Technical validation required.
ISO: S · Geometry: D6 | R3 | Z4
Technical validation required
View datasheet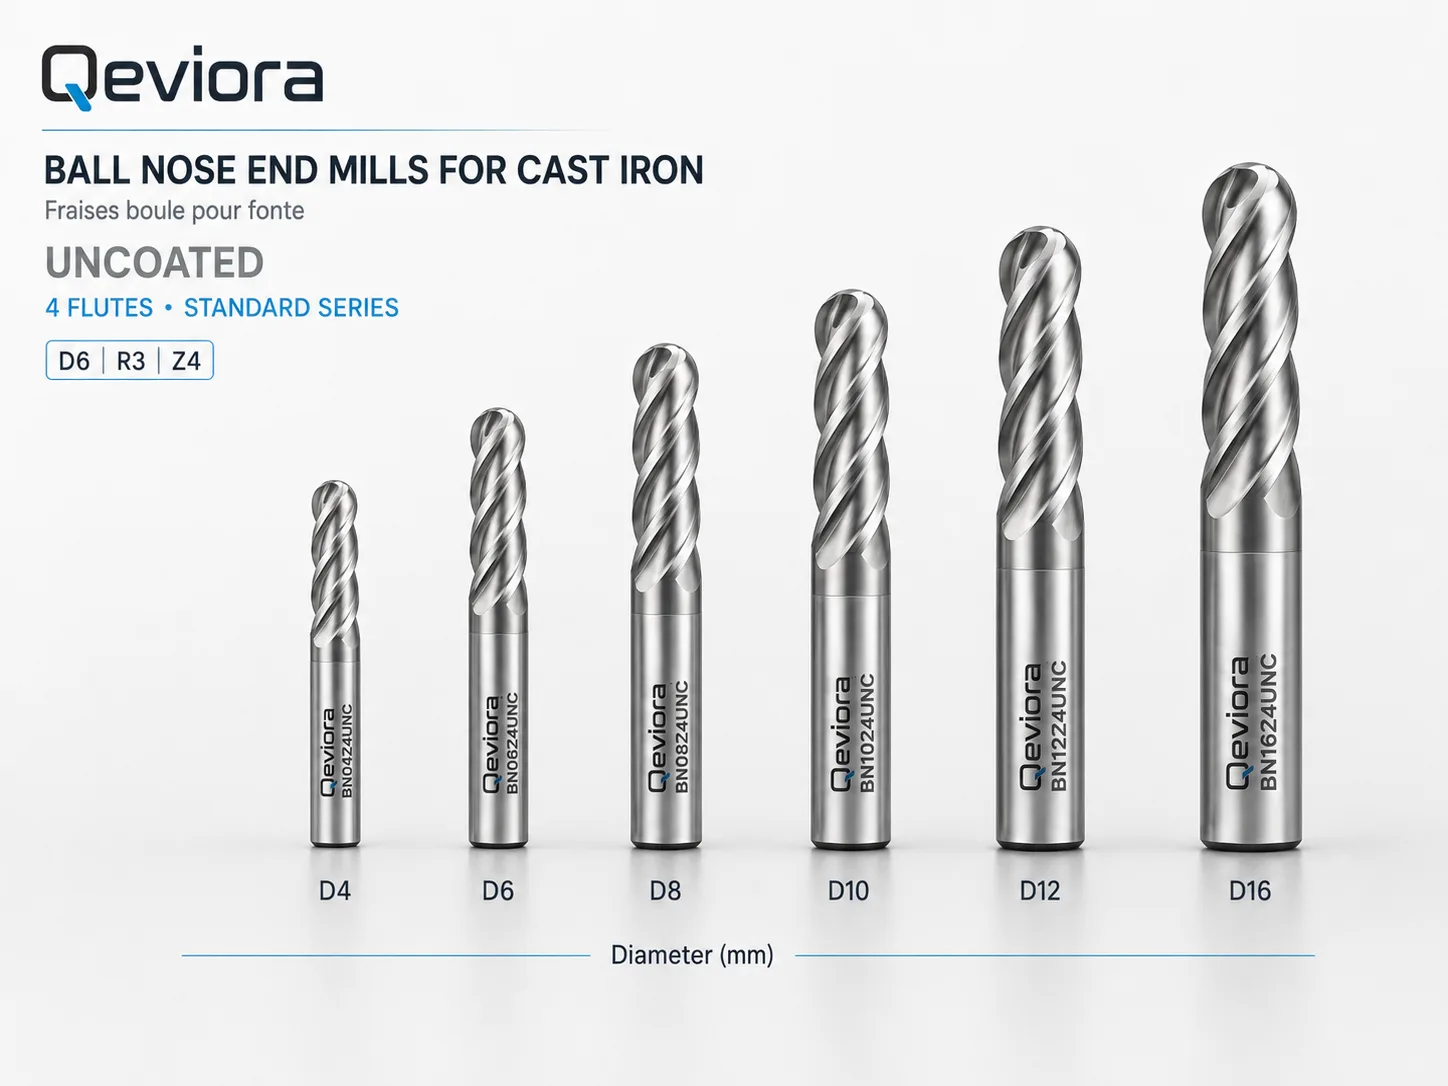
Cast iron
Cast Iron
Grey, nodular and alloyed cast irons — ISO K, uncoated visual finish.
ISO: K · Geometry: D6 | R3 | Z4
View datasheet
Applications
3D machining and contour finishing
Select the family by material and operation. Images illustrate ball-nose geometry; they do not replace shop-floor validation.
- 3D surfaces and complex shapes
- Moulds, dies and cavities
- Contours, radii and semi-finishing
- Consistent finishing in difficult-to-reach areas
Cutting conditions
Indicative starting values — tool D6, R3
Conservative starting ranges for a D6 ball nose with low to moderate radial engagement. Confirm by trial.
Structure and logic derived from ISO classification and public Walter recommendations; provisional Qeviora values pending validation.
| Family | ISO | Initial vc (m/min) | Initial fz (mm/tooth) | Recommended ae | Recommended ap | Cooling |
|---|---|---|---|---|---|---|
| General Purpose | P/M/K | 70–140 | 0,015–0,035 | 3–10 % D | 0,05–0,30 D | Air or emulsion |
| Aluminum and Non-Ferrous Materials | N | 250–500 | 0,025–0,060 | 5–15 % D | 0,10–0,50 D | Air, MQL or emulsion |
| Steel | P | 80–150 | 0,015–0,035 | 3–10 % D | 0,05–0,30 D | Air or emulsion |
| Stainless Steel | M | 45–90 | 0,012–0,030 | 3–8 % D | 0,05–0,25 D | Emulsion recommended |
| Hardened Steel | H | 35–90 | 0,008–0,025 | 1–5 % D | 0,02–0,15 D | Clean air / stable strategy |
| Titanium and Heat-Resistant Alloys | S | 35–70 | 0,010–0,025 | 2–6 % D | 0,05–0,20 D | Abundant, reliable coolant |
| Cast Iron | K | 90–180 | 0,015–0,040 | 3–10 % D | 0,05–0,30 D | Dry / extraction or process-dependent |
In ball-nose milling, effective cutting speed decreases toward the tool centre. For 3D finishing, prefer tool tilt or a toolpath that avoids continuous centre cutting.
Parameter calculator
Starting aid only. Does not replace shop-floor validation.
- Spindle speed n
- 5,305 rpm
- Feed rate Vf
- 424 mm/min
Reduce values for long overhang, low rigidity, runout, unfavourable interpolation or higher engagement.
Method
How to choose
A progressive selection reduces unnecessary trials and protects the tool.
- 01Identify the main ISO material group (P, M, K, N, S, H).
- 02Select the matching visual family and check validation status.
- 03Start from indicative D6 | R3 values, then adjust for rigidity, overhang and engagement.
- 04Avoid permanent centre-cutting of the ball during 3D finishing.
- 05Confirm by trial before industrialisation.
Technical warning: illustrated visuals, coatings and cutting parameters are indicative only. They are not a performance guarantee, a commercial equivalence with another manufacturer, or final validation without machine trials.

Kontakt
Sprechen wir über Ihr Industrieprojekt
Unser Team ist verfügbar, um Ihre Herausforderungen zu verstehen und eine Begleitung passend zu Ihren Leistungszielen vorzuschlagen.
(+212) 06 38 38 11 46
Telefon
(+212) 06 38 38 11 46
admin@qeviora.com
Angebot
devis@qeviora.com

Website
www.Qeviora.com
Standorte
Qeviora Präsenz
Unsere strategische Präsenz für Ihre Nähe.
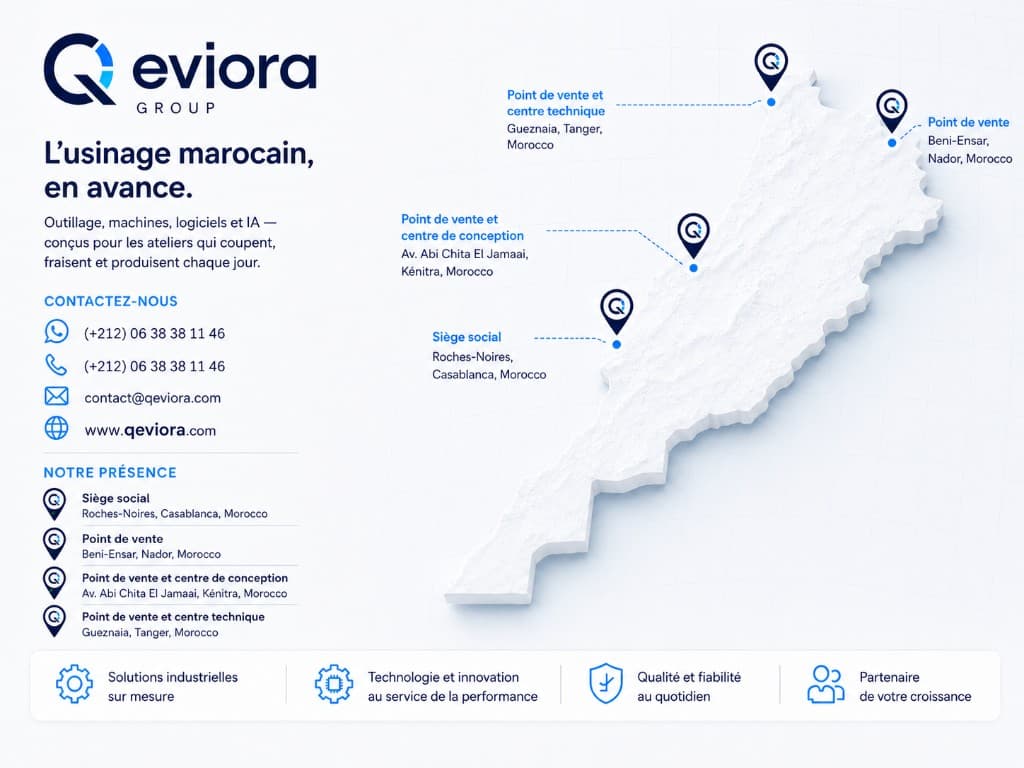
Hauptsitz
Roches-Noires, Casablanca, Morocco
Verkaufsstelle und Designzentrum
Av. Abi Chita El Jamaai, Kénitra, Morocco
Verkaufsstelle und Technikzentrum
Gueznaia, Tanger, Morocco
Verkaufsstelle
Beni-Ensar, Nador, Morocco